tire-manufacturing-logo-512
Tire manufacturing

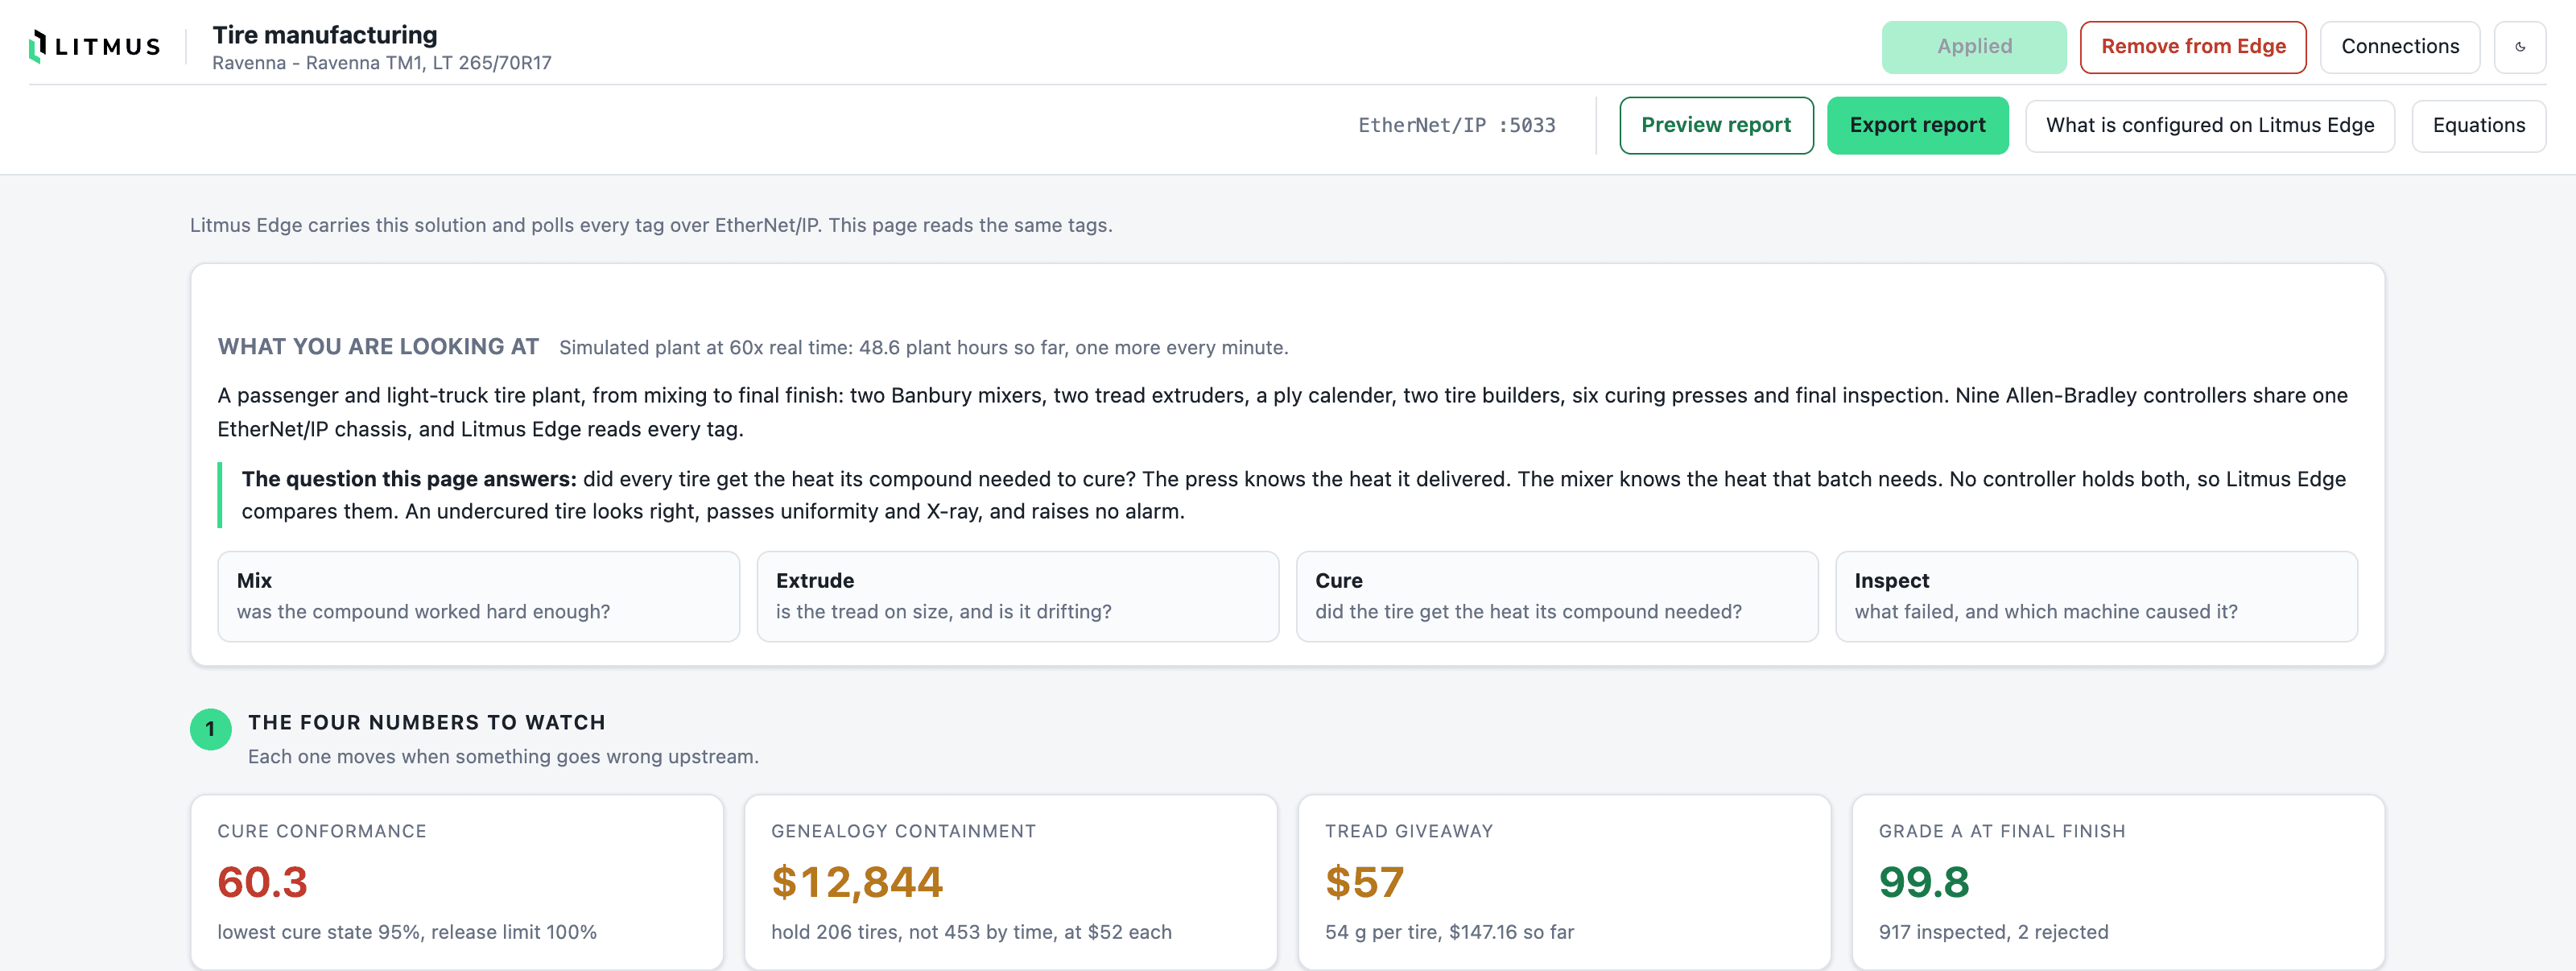
A tire plant from the mixing room to final finish over EtherNet/IP, where a batch mixed on time instead of energy leaves tires that look right and are undercured.

v0.5.1

How it works

What it simulates

A passenger and light-truck tire plant from the mixing room to final finish: two Banbury mixers, two tread extruders, a ply calender, two tire builders, a bank of six curing presses and final inspection. Nine Allen-Bradley controllers on one ControlLogix chassis, 357 tags over EtherNet/IP.

It is batch, continuous and discrete in one material flow. How well a compound was mixed is a batch property, carried by a green tire into the cure, and the press never learns which compound it holds. Litmus Edge joins the two.

  • an isometric floor that follows the material, with a suspect batch shown in red wherever it has reached
  • the machine view, and the digital twin of any machine on a click

What it configures on Litmus Edge

On startup, and it removes exactly what it created when you are finished:
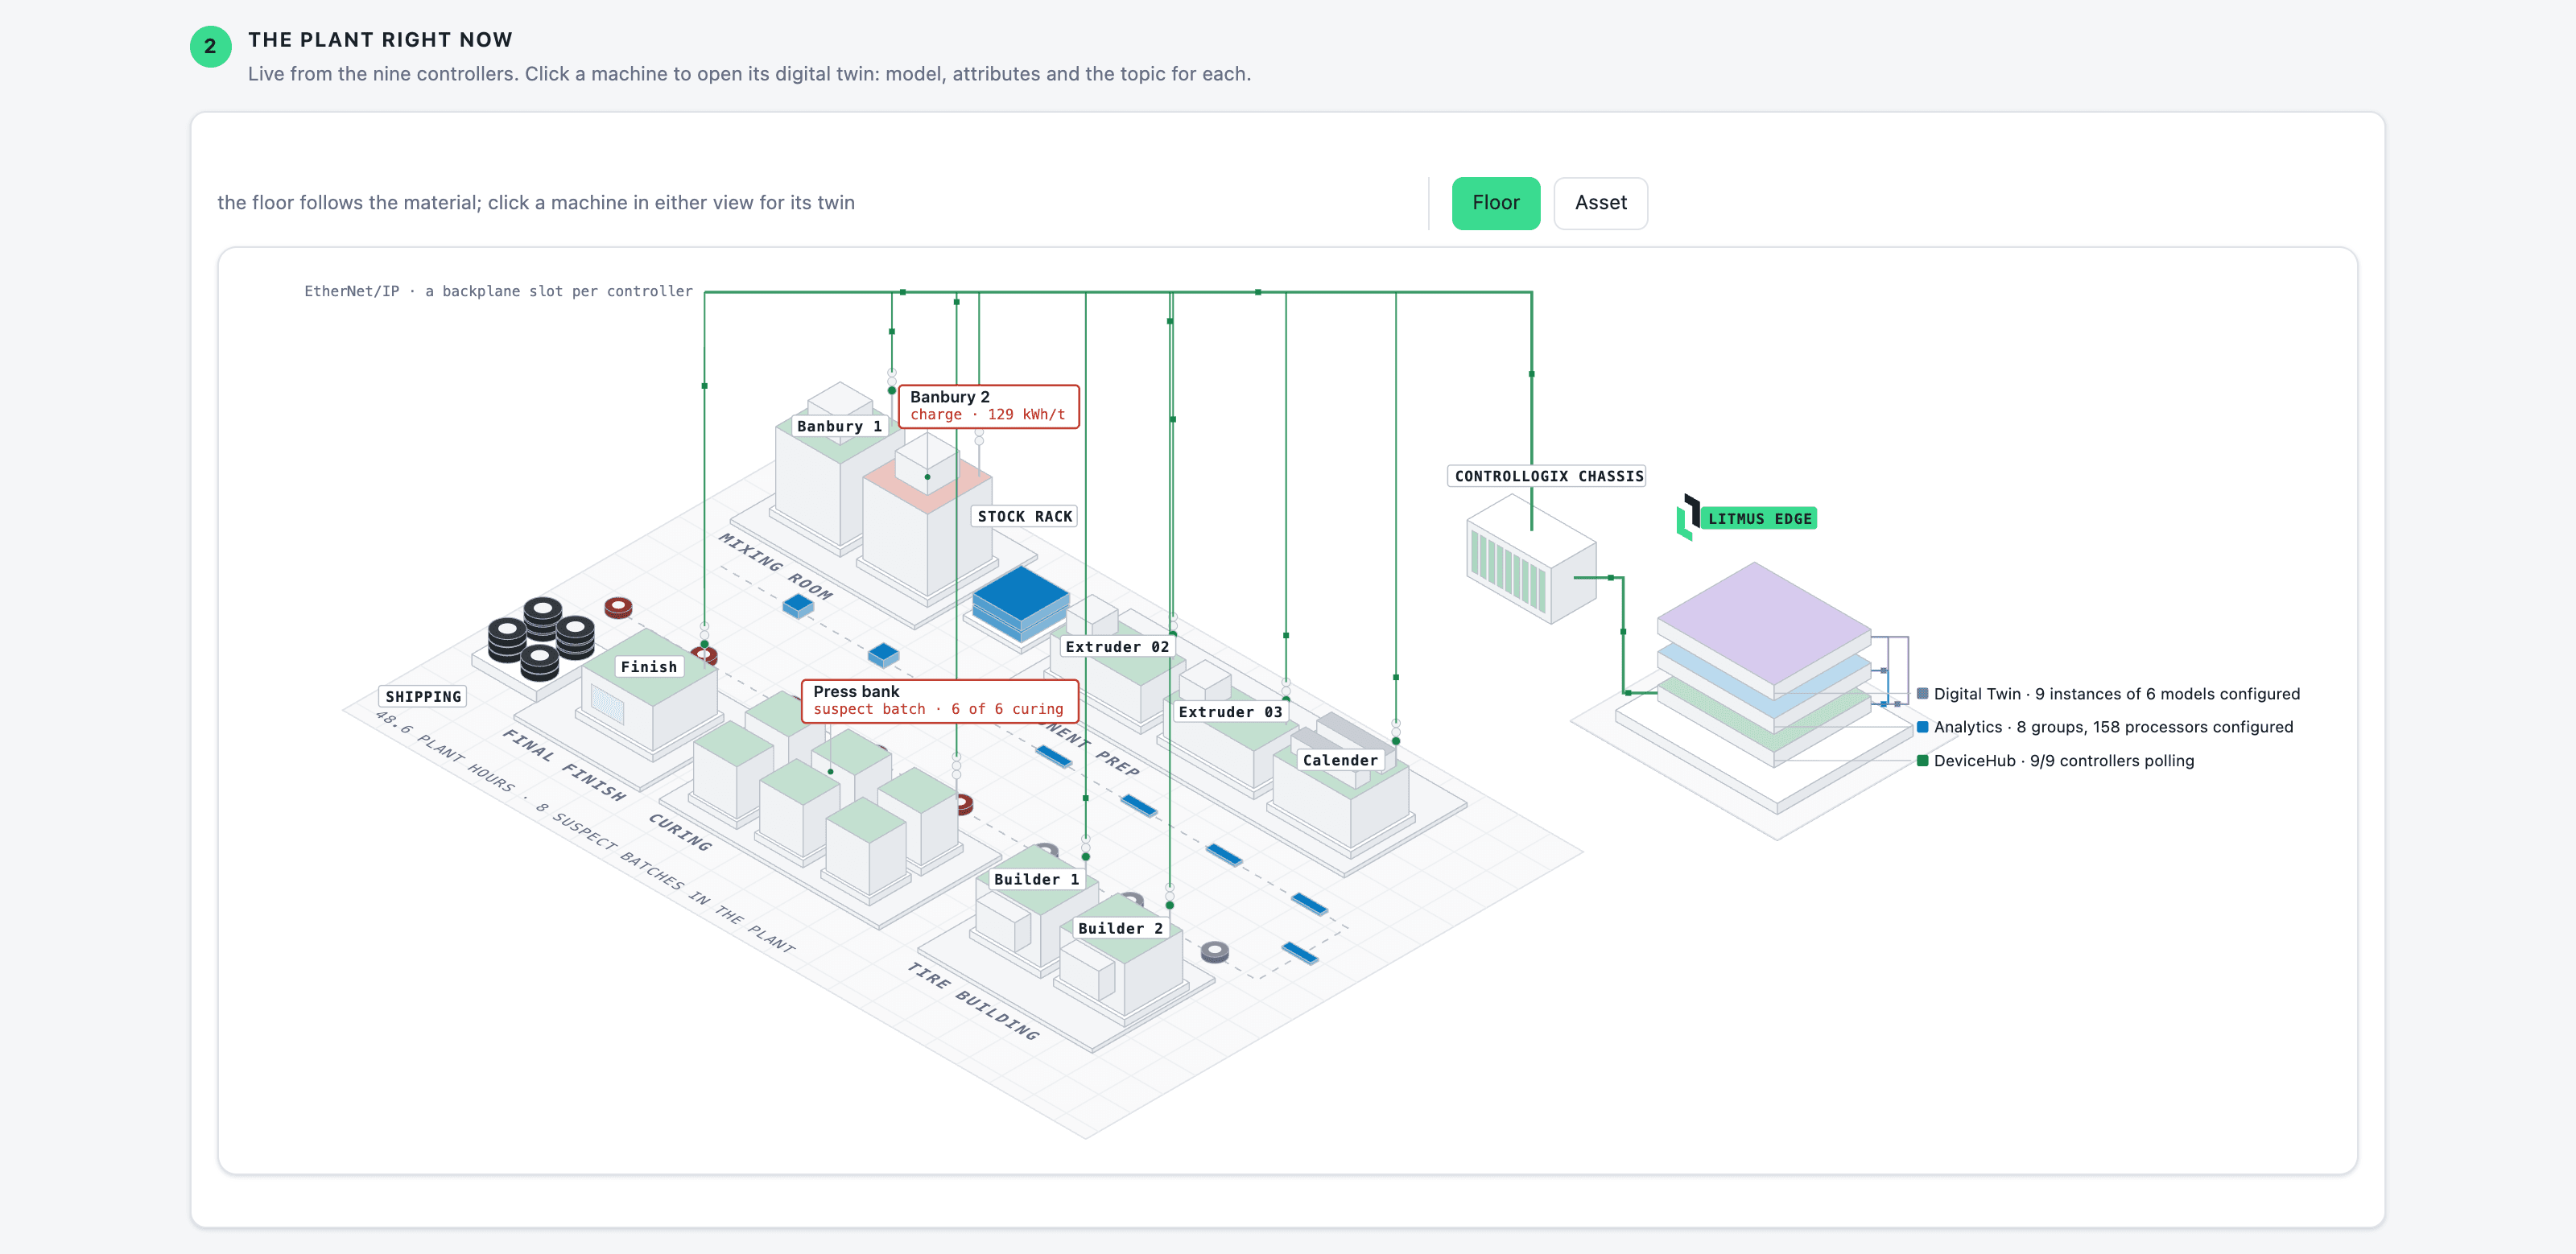
  • 9 DeviceHub devices on the AB Logix Ethernet driver, one backplane slot each
  • 6 Digital Twin models with 9 instances
  • 8 Analytics groups, among them cure state verification, compound quality, tread giveaway and process capability by die cavity

Scenarios you can inject

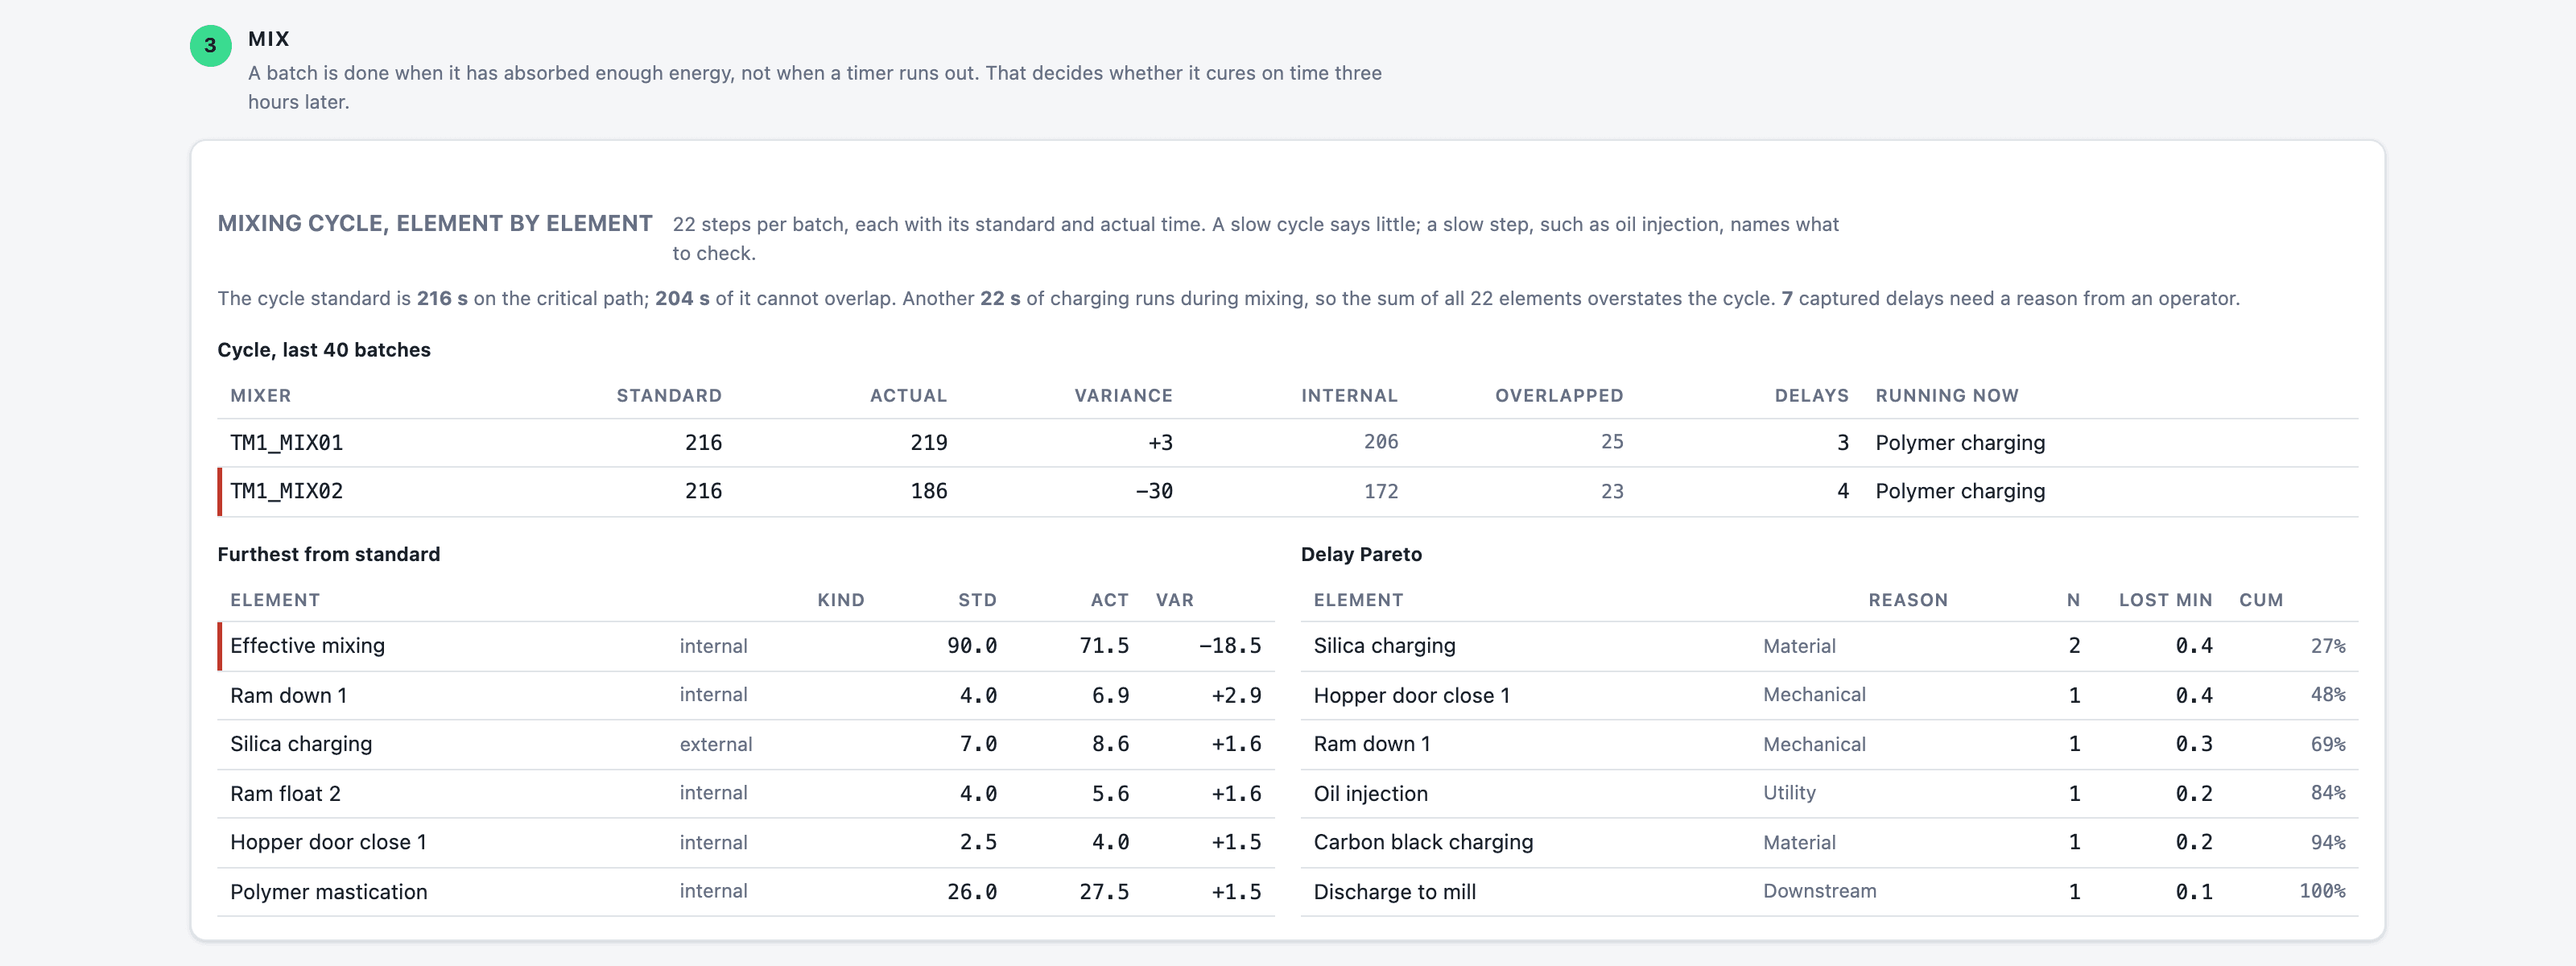
  • A Banbury dropping on time instead of energy leaves tires that pass uniformity and X-ray and are undercured
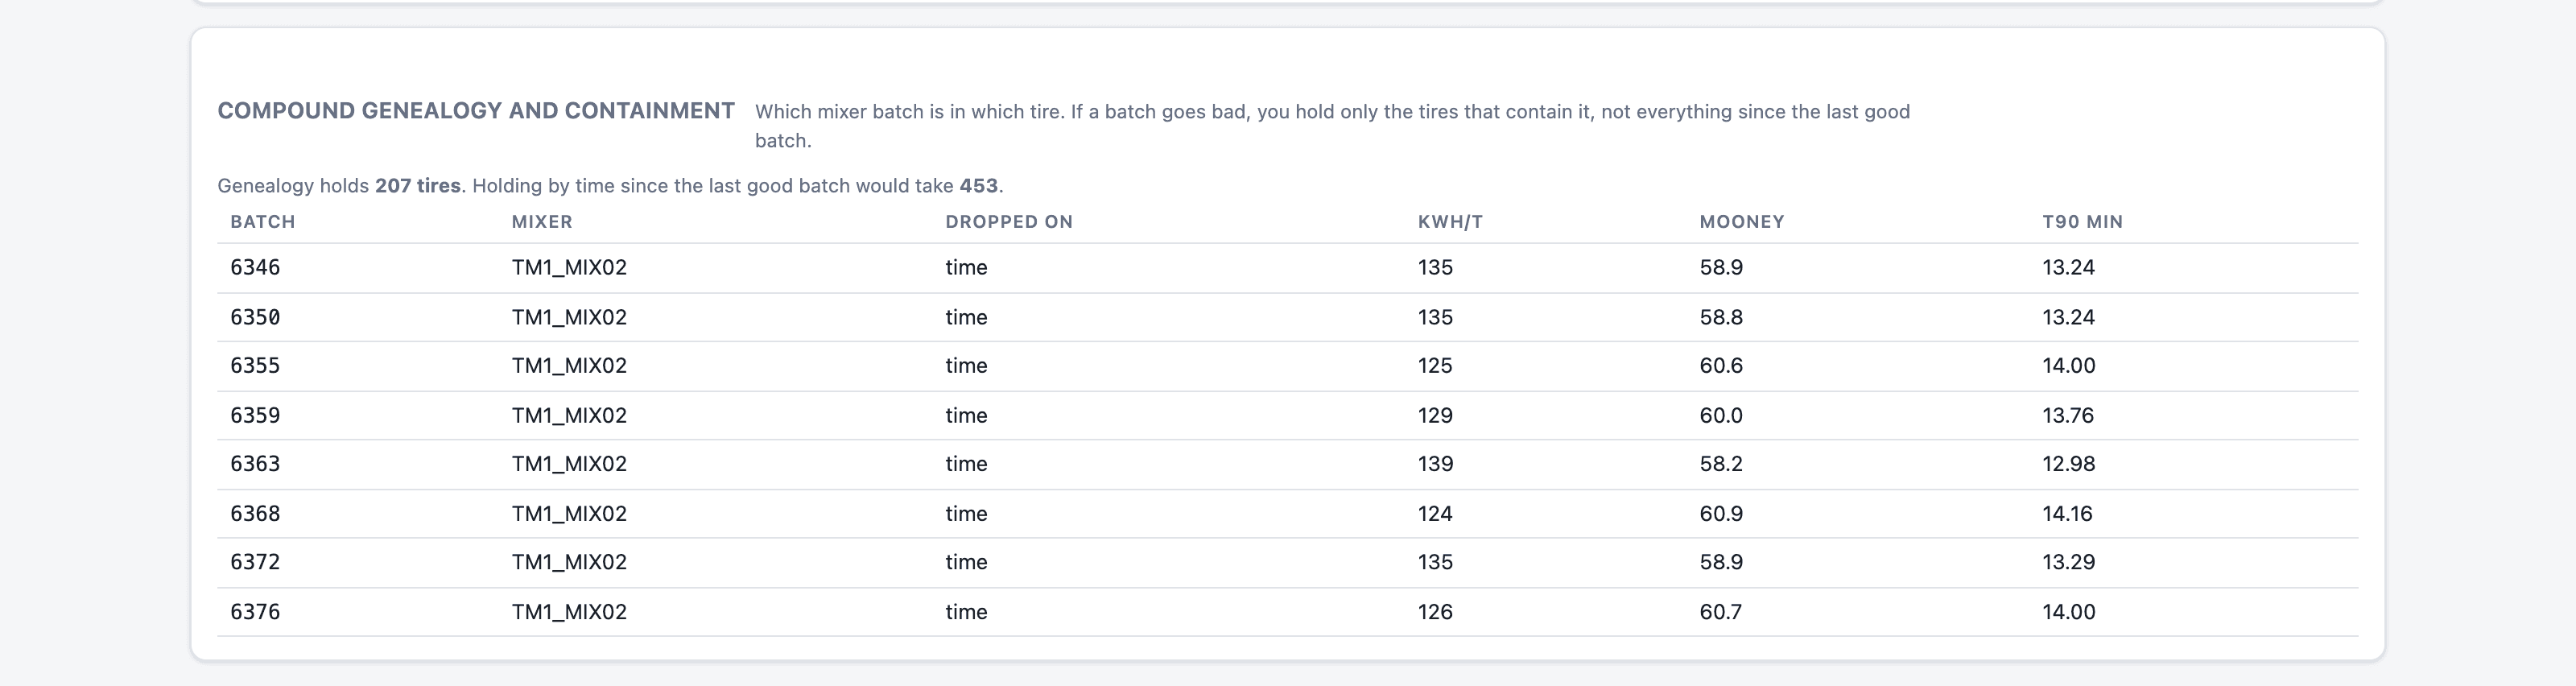
  • Containment by genealogy holds a fraction of the tires that holding by the clock would
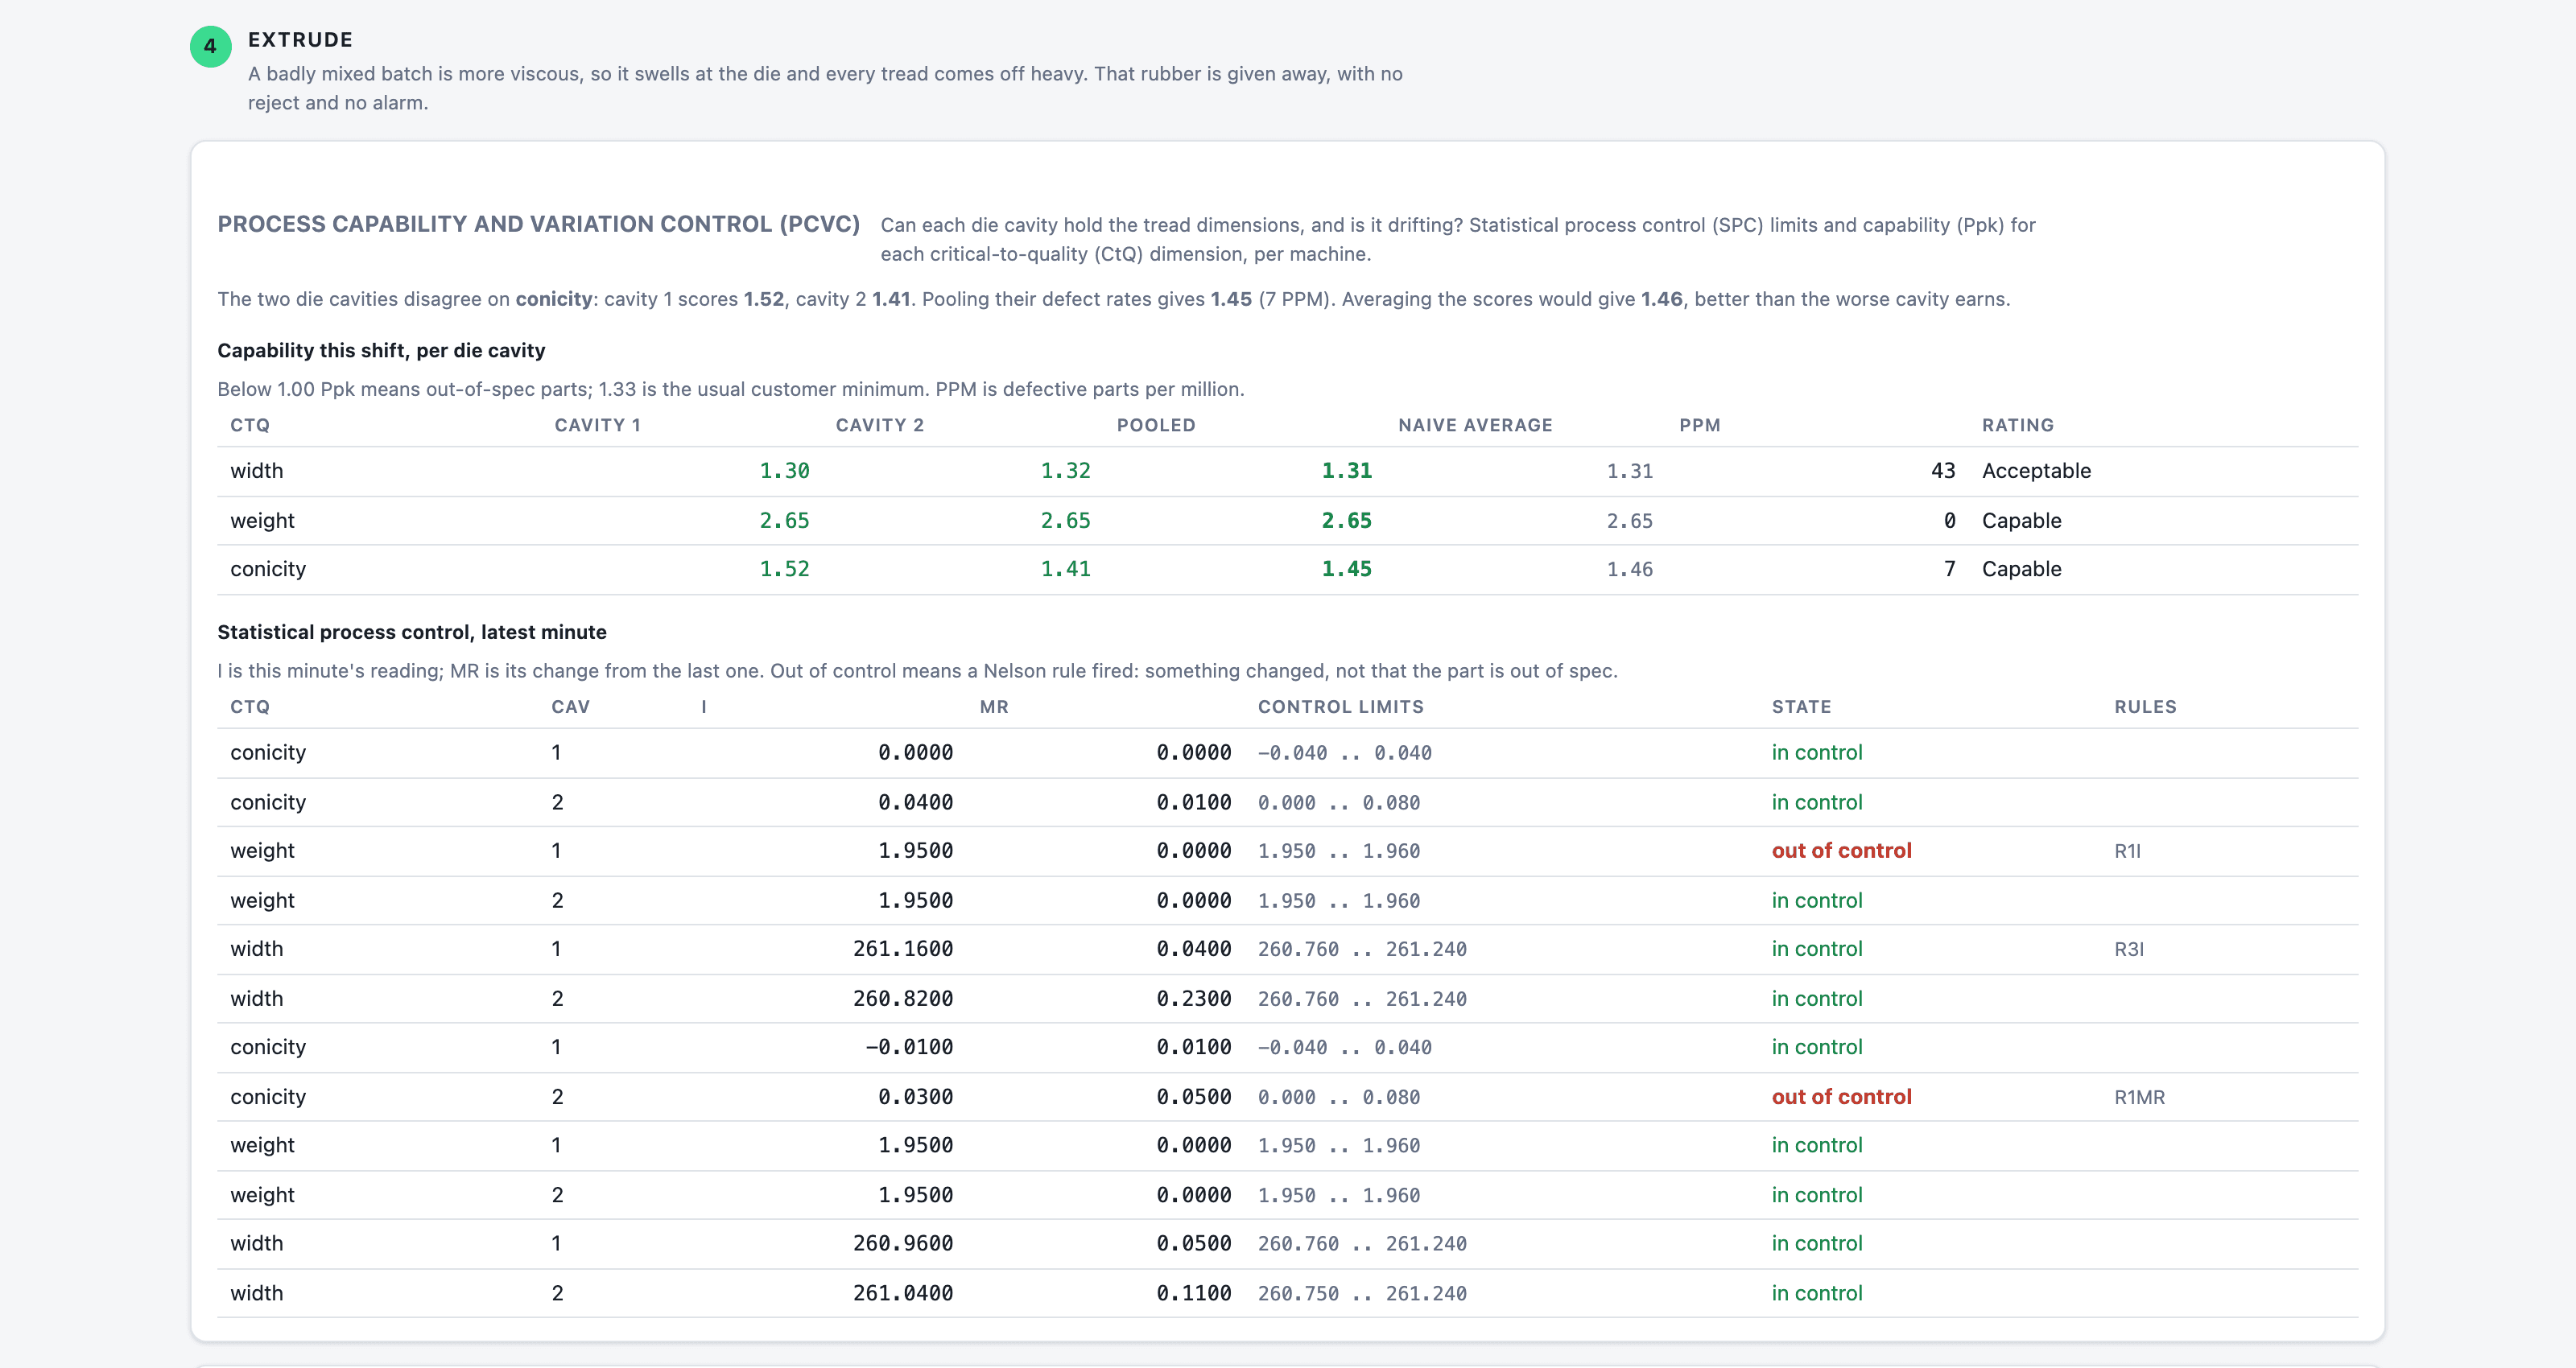
  • The same compound runs heavy at the extruder, so the plant ships free rubber with nothing rejected
  • A failing steam trap on one press undercures too, and where the undercures fall tells the two causes apart
Tire manufacturing: The plant floor, with a suspect batch moving through it
Tire manufacturing: The four numbers to watch
Tire manufacturing: The mixing cycle, element by element
Tire manufacturing: Compound genealogy and containment
Tire manufacturing: Process capability by cavity